Every shop that taps holes eventually asks the same question, and the thread that usually settles it is a small-fabrication scenario: someone on r/metalworking wants to tap M6 to M10 in 5/8 inch A572 steel and is deciding whether their drill press can survive it. That question drives this roundup of the best tapping machines for metalworking in 2026.
The short answer is that a drill press can do it, but slowly, and only with a rigid setup, cutting oil and very steady feeds. A dedicated tapping machine feeds the tap into the hole at exactly the rate the tap advances, then reverses at the same speed, which is why it produces repeatable threads and far fewer snapped taps.
We compared 12 tapping arms, pneumatic tappers and one live-pipe tapping kit, working from their spec sheets, build details and buyer feedback. Everything below is written for a small shop or job shop that wants predictable threads rather than a production line that wants cycle time.
Table of Contents
What Is a Tapping Machine?
A tapping machine is a purpose-built machine that cuts internal screw threads into predrilled holes by driving a tap at a synchronized, controlled speed and torque. It grips the tap in a floating tap holder or torque collet chuck, spins it forward at a fixed cutting speed, and feeds it into the hole at exactly the rate the tap advances itself. When the tap reaches set depth, the machine reverses at identical speed to withdraw it and cut the thread backward on the way out.
That synchronization is the whole point. A drill press or hand wrench pushes the tap faster than the tap cuts, which loads the cutting edges sideways and shears them. Buyers consistently tell us the machine they value most is the one that does not break taps, not the one with the highest headline speed.
Two terms matter when you read specs. A torque collet chuck slips when torque exceeds a set value, protecting the tap. A floating tap holder allows the tap to follow its own pitch. Machines that have neither give you no protection at all, which is why we note that gap in every review below.
What Are the Different Types of Tapping Machines?
There are seven machine classes you will meet in a metalworking shop, and each one has a clear job. Knowing which class you need is the fastest way to shortlist a purchase.
Electric tapping arm – a floor or bench-mounted swing arm with a servo motor and touch panel, typically M3 to M16 or M3 to M24. The default choice for a small fabrication shop. Not suited to tapping without first drilling.
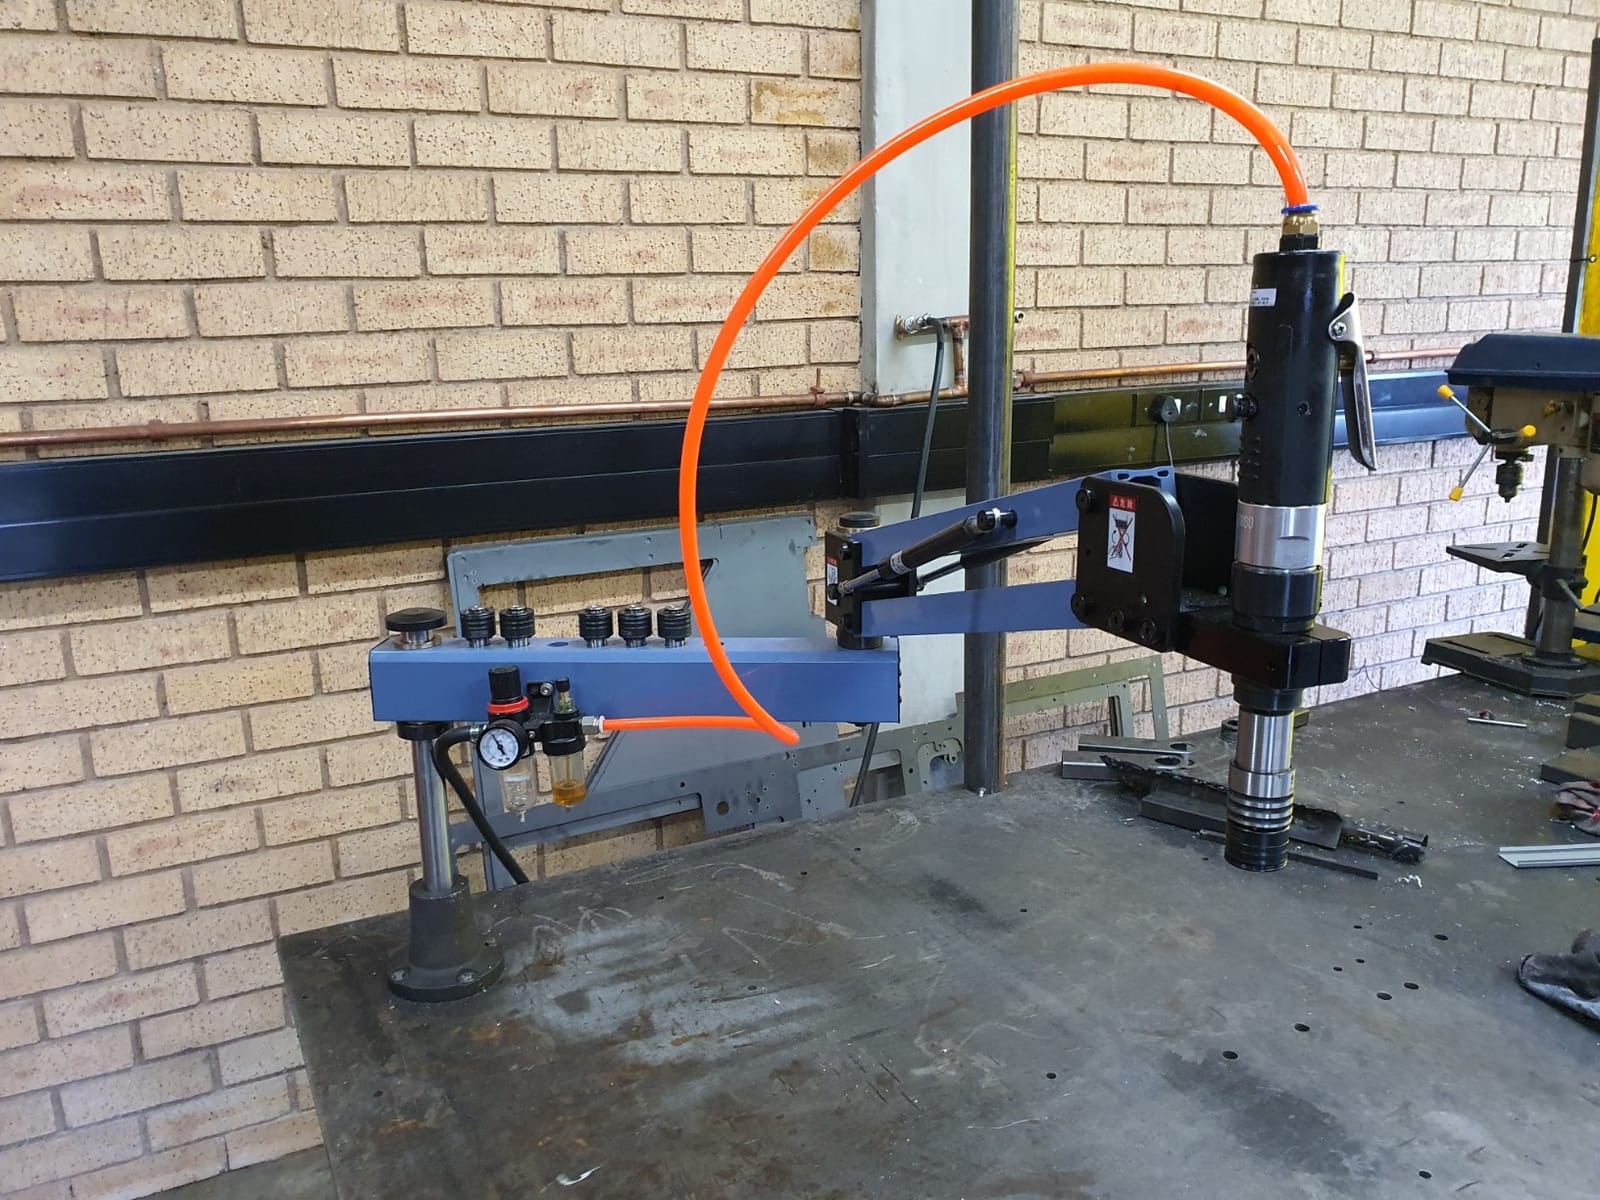
Pneumatic tapping arm – the same swing-arm format driven by shop air, usually M3 to M12. Cheaper and simpler, with a safety clutch on better models. Not suitable for hardened alloys and limited on large threads.
Pneumatic tapping gun – a hand-held air tool you mount to an articulating arm you already own. Entry-level capacity, no torque protection on most models. Not a complete machine on its own.
Bench or tabletop tapping machine – a compact vertical unit fixed to a bench, useful when every job is a vertical hole. Not useful for overhead or side-facing work.
CNC drilling and tapping center – a gantry machine with rigid tapping, an automatic tool changer and programmable depth. The right answer for batch volume. Overkill and expensive for occasional work.
Magnetic-base tapping machine – a portable unit that clamps to steel by magnetic force for field and jobsite work. Requires a ferromagnetic plate and will not hold on thin or non-magnetic stock.
Tapping head retrofit – a head that mounts on a mill or drill press spindle to add synchronized tapping to a machine you already own. Adds capability only if your existing spindle is rigid enough.
Note what each class is not good for. A flexible arm cannot give you CNC-level positional repeatability. A benchtop unit cannot reach into a fabricated box. A retrofit head cannot fix a spindle that flexes. Buyers on cnczone and polytechforum draw the same line between a mill-mounted tapping head for volume work and a standalone arm for flexible, low-volume work.
Top 3 Picks for Metalworking Tapping (September 2026)

WTTTOOLS M3-M16 Electric Arm
- Three tapping modes
- 0-375 r/min
- One-year warranty
- Nine-piece collet set

Best Tapping Machines for Metalworking in 2026
Here is the full field in one view. Tap capacity and speed are the first filter; drive type and torque protection decide whether the machine will still be working for you in a year.
| Product | Specifications | Action |
|---|---|---|
| XINCHENG M3-M16 Electric Tapping Arm |
|
Check Latest Price |
| WTTTOOLS M3-M16 Electric Tapping Arm |
|
Check Latest Price |
 Generic M4-M24 Electric Tapping Arm |
|
Check Latest Price |
 Generic M3-M16 Electric Tapping Machine |
|
Check Latest Price |
 TECHTONGDA M3-M16 Electric Tapping Machine |
|
Check Latest Price |
 INTBUYING M3-M16 Vertical Electric Tapper |
|
Check Latest Price |
 Pavrots M6-M36 Electric Tapping Arm |
|
Check Latest Price |
| MXBAOHENG Pneumatic Tapping Gun |
|
Check Latest Price |
 TX Pneumatic Tapping Arm 1000mm |
|
Check Latest Price |
 Sevencow Mechanical Hot Tapping Kit |
|
Check Latest Price |
 DEJUN Pneumatic Tapping Machine |
|
Check Latest Price |
 LYXC M6-M36 Electric Tapping Machine |
|
Check Latest Price |
1. XINCHENG PRECISION M3-M16 Electric Tapping Arm – Best Overall for Small Shops
US Stock M3-M16 Universal Electric Tapping Machine Electric Tapping Arm with 375rpm 1200mm Flexible Tapping Arm included 9pcs ANSI Standard Collets
Capacity: M3-M16
Speed: 0-375 rpm
Motor: 600W servo
Reach: 1045mm horizontal
Pros
- Commercial-grade coatings on all surfaces
- Crates in a solid timber crate with steel edge reinforcing
- Touch panel makes setup quick
- Has a solid mounting point for rigid bench use
- Automatic reverse plus safety torque collet
Cons
- Collets can arrive sticky and need cleaning
- Imperial sizes given as inch fractions not US screw sizes
- No drilling function
This is the machine we would put in a small fabrication shop that taps M3 to M10 all week and occasionally stretches to M16. It runs 110V, steps speed steplessly from 0 to 375 rpm, and covers a 1045mm horizontal by 400mm vertical working area from a 360 degree workhead.
All six ratings on this listing are five stars. Buyers single out the commercial-grade coatings on every surface, the timber crate with steel edge reinforcing, and how quickly the touch panel gets someone running. One reviewer describes it as a professional tool in every respect and confirms the mounting point is solid for rigid bench or fixture work.
What earns it the top slot is the combination of torque protection and reach. The safety torque collet with overload protection means a hard thread stops the collet rather than snapping the tap, and the automatic reverse handles the withdrawal stroke. That is the specific failure machinists worry about most.
The honest catch is regional fit. Imperial size selections are given in inch fractions rather than US screw designations, which is confusing if you think in #6-32 and 1/4-20. Collets can also arrive sticky and need cleaning before first use. And it taps only, so you still need a separate way to drill the pilot holes.
Why it suits a small fabrication shop
At 77.2 pounds it is heavy enough to stay put on a bench and light enough that one person can reposition it. The 1045mm reach covers most bench work without needing the arm swung around a corner.
If your work is M6 through M10 in mild steel or aluminium, this is the sweet spot of the whole list. Set the speed, set the depth, and the machine repeats the cycle identically every time.
Where it will frustrate you
It will not drill. Every job starts with a pilot hole from a drill press, and a shop that never pre-drills will outgrow this machine fast.
Anyone tapping imperial fasteners on a US bench should confirm the thread labelling matches their habits before committing, because the interface cannot be relabeled.
2. WTTTOOLS M3-M16 Electric Tapping Arm – Best for Repeated Production Work
US Stock M3-M16 Electric Tapping Machine Tapper Tapping Arm Universal 360 Degree 9PCS ANSI Collets Included
Capacity: M3-M16
Speed: 0-375 r/min
Motor: 600W servo
Reach: 1045mm horizontal
Pros
- One buyer cut tapping time by 50 percent
- Keeps taps straighter so fewer break
- Digital screen makes programming straightforward
- Works across aluminum stainless and carbon steels
- One-year warranty on the whole machine
Cons
- Collets arrive sticky and need brake cleaner
- Imperial sizes listed in inches and cannot be relabeled
- No drilling function
- 110V units can trip a GFCI without a transformer
This machine has the largest body of written user feedback in the group, 12 reviews averaging 4.6 stars, and the feedback is about output rather than specification. A machine-shop buyer reports cutting tapping time by half and says it paid for itself in about five months. Another says the tap stays straighter, so fewer taps break on custom and one-off work.
The spec sheet supports those claims. It runs 0 to 375 r/min on a 600W servo, offers manual, automatic and deep hole tapping modes, and lets you adjust speed, depth and torque independently on the digital screen, with forward and reverse speed both adjustable. The material list is broad, covering aluminium, copper, A3 steel, 45 steel, cast iron, Q235, S136, mold steel, 718H, 40Cr and stainless steel.
It ships with a nine-piece GT12 ANSI torque collet set covering 1/16 inch through 1/2 inch, which is a better imperial spread than most of the electric arms here. The whole machine carries a one-year warranty, and at 69.9 pounds it is one of the lighter frames in the group.
The criticism buyers raise most is regional fit again. Imperial thread options are listed in inches rather than US screw sizes, and the interface does not let you rename the labels. One buyer also hit a tripping GFCI outlet on 110V, which the manufacturer resolved by shipping a transformer from China. Collets arrive sticky and want brake cleaner before use.
Why it fits a busy job shop
The automatic and deep hole modes are the reason this one rates well with repeat work. Deep hole mode is a real feature on a machine at this level, and few competitors in this price bracket offer it.
Being able to tune reverse speed independently matters on stainless and aluminium, where an aggressive withdrawal can grab and tear the thread. Buyers running mixed material appreciate that.
Where you may want something else
If your work stops at M12, this is more machine than you need. If you tap 1/4 inch or larger imperial fasteners by designation, the labelling will slow you down at the panel every time.
It also cannot drill, so budget the pilot-drilling step into your cycle time rather than assuming one machine does both.
3. Generic M4-M24 Electric Tapping Arm – Wider Range for Structural Work
US Stock M4-M24 Electric Tapping Machine Tapper Tapping Arm 360° Universals Tappings Machine 200rpm 1180mm Flexible Tappings Arm Included 9PCS ANSI Standard Collets
Capacity: M4-M24
Speed: 0-200 rpm
Motor: 1200W servo
Reach: 1180mm horizontal
Pros
- Covers M4 through M24 in one machine
- 1200W output with double torque protection
- 1180mm reach and 550mm vertical range
- Manual automatic and batch processing modes
- Exceptionally responsive seller support
Cons
- Torque clutch sits on the tool holder so it must be reset per tap size
- Clutch needed repeated adjustment during one project
- Generic listing with placeholder specification fields
Most electric tapping arms stop at M16. This one runs M4 to M24 on a 1200W servo with stepless 0 to 200 rpm regulation, which makes it the answer when a job needs a structural thread and your other machines cannot reach it. It is the widest mid-range capacity in this roundup, and it stops well short of the M6 to M36 machines further down.
The reach is unusually long at 1180mm horizontal and 550mm vertical, so you can reach across a bench or into a frame without moving the base. It supports manual, automatic and batch processing, and the touch screen exposes digital speed, feed rate and depth settings along with an automatic reversal device and a safety torque chuck.
Both reviews on this listing are five stars and talk about results rather than numbers. One buyer says it keeps holes consistently vertical in a way hand tapping could not guarantee, and started tapping joints where they previously welded. Another notes the time saved on repetitive work. Seller support was singled out after an out-of-spec collet was replaced.
The catch is real and specific: the torque clutch lives on the tool holder rather than the motor, so it has to be re-adjusted for every tap size. One buyer found themselves adjusting it repeatedly during a single project. The listing is also sold as Generic with placeholder fields, so expect less documentation than a branded machine.
Why it earns its place
M20 and M24 threads appear in structural steel, machine bases and hydraulic manifolds, and almost no affordable arm covers them. Having one machine for M4 through M24 removes the temptation to hand-tap the large end.
The 1200W motor also gives it more headroom than the 600W arms, which matters when you are cutting a coarse-pitch thread in A572 or 45 steel.
Where it falls short
That per-tap clutch reset is a genuine workflow tax. If you alternate between sizes on every part, you will be turning an adjuster constantly, and a clutch that is set too high still snaps taps.
Only two reviews exist, and the placeholder spec fields mean you are relying on the description rather than a documented datasheet. Ask the seller for the clutch procedure before you commit.
4. Generic M3-M16 Electric Tapping Machine – Clean Setup for Fabricators
Electric Tapping Machine Metalworking Shops M3-M16 600W Servo Tapper
Capacity: M3-M16
Speed: 0-375 RPM
Motor: 600W servo
Reach: 1045mm horizontal
Pros
- Large time saving on repetitive holes in small-batch work
- Keeps the tap straighter than hand tapping
- Arm moves smoothly and stays stable
- Ten GT12 ANSI torque collets from 1/4 to 15/16 inch
Cons
- Very new listing with almost no independent user history
- Sold as Generic with placeholder specification fields
This is the straightforward M3 to M16 arm for a fabricator who taps the same few hole sizes over and over. It runs on 110V with a 600W servo at 0 to 375 RPM, and the digital panel sets tapping speed, return speed, depth and torque independently.
Two five-star reviews come from fabrication shops doing repetitive work, and they converge on the same conclusion. One describes a large time saving on small-batch jobs with a smooth, stable arm. The other says that for repetitive work there is no comparison to hand tapping, and calls it more useful if you fabricate regularly.
The feature list is the reason to look closely. Servo control overload protection is described as reducing tap breakage across through-hole, blind-hole and deep-hole work, and forward and reverse speeds are adjustable for cleaner threads. Ten GT12 ANSI torque collets cover 1/4 inch through 15/16 inch, which is the widest imperial collet spread on an M16 machine here.
Be honest about the evidence, though. The listing only became available recently and carries two reviews, so there is essentially no long-term durability history to judge. It is also sold as a Generic brand with placeholder specification fields rather than a documented datasheet.
Why a fabricator would buy it
Adjustable return speed is the feature most people underrate. On aluminium and 304 stainless, an aggressive withdrawal is what grabs and breaks taps, and being able to slow the reverse separately makes a measurable difference.
The collet spread means you can cover imperial work from 1/4 inch up without buying a second collet set.
Where caution is warranted
Two reviews is not a service record. If your shop depends on this machine daily, factor the unknowns into your decision and keep a hand tap and a spare collet set on the shelf.
It taps only, and the head does not drill, so the pilot hole step stays manual no matter how much you automate the rest.
5. TECHTONGDA M3-M16 Electric Tapping Machine – Highest Published Torque
TECHTONGDA M3-M16 Electric Tapping Universal 360 Angle Electric Touch Tapping Machine for Machinery Manufacturing Industry Drilling Machine 220V 600W (M3-M16)
Capacity: M3-M16
Speed: 156 rpm, 312 max
Torque: 256 N m
Motor: 600W
Pros
- Highest published torque in the electric group
- Double torque protection with preset machine torque
- Copper sleeve and bearing parts for tapping accuracy
- Also drills up to 16mm in metal
Cons
- 220V supply requires a step-down transformer on US circuits
- No written user review to judge real-world performance
If torque is what you are short of, this machine publishes 256 N m, the highest figure in the electric group here, from a 600W motor running at 156 rpm with a maximum rotational speed of 312 rpm. That headroom is what lets it tap coarse threads in tougher steel without stalling.
Two protection systems are specified: preset machine torque plus double torque chuck protection. The rotating parts use a graphite copper sleeve and bearing, which the manufacturer credits for tapping accuracy and flexible rotation. The material coverage is broad, spanning A3 steel, 45 steel, cast iron, pig iron, Q235, S136, 718H, 40Cr and stainless steel.
One detail separates it from most of the other arms: it also drills. The listed metal drilling capacity is 16 millimeters, so a shop that does not own a separate drill can at least form pilot holes on the same machine.
Two cautions. It runs on 220V, so a US shop needs a step-down transformer before it will power up. And it carries a single five-star rating with no written review, which means the assessment here rests on the specification sheet alone rather than on owner testimony.
Why torque is the deciding spec
Torque is what separates a machine that taps from a machine that stalls. When the torque clutch is set properly, torque headroom means the clutch protects the tap instead of the drive balking the cycle halfway down the hole.
If you cut steel regularly, especially 45 steel or 718H, the 256 N m figure gives more margin than the 200 N m machines at the same motor wattage.
Where it will not suit
The 220V supply is the practical blocker for most US shops. Budget for a transformer and confirm the outlet amperage before you commit.
With no written user review, you are buying on spec. Ask for a demonstration on your own material before you sign off on it.
6. INTBUYING M3-M16 Vertical Electric Tapper – Best for Vertical Bench Work
INTBUYING Electric Tapping Threading Machine M3-M16 Vertical Type Servo Tapper Drilling Machine 600W Stepless Speed Intelligent CNC Desktop Swing Arm AutomaticTtapping Machine 220V
Capacity: M3-M16
Speed: 156 rpm
Torque: 200 N m
Motor: 600W
Pros
- Integrated aluminum alloy structure cuts overall volume
- Touch-screen panel with a clear interface
- High strength body improves precision and stability
- Accepts standard tap collets including non-clutch collets
Cons
- 220V supply requires a step-down transformer
- 200 N m is less torque headroom than the 256 N m machine
- Only one review gives limited reliability evidence
This machine is built around an integrated aluminum alloy support structure that positions the control panel and tapping collet together on the upper shell. The result is a smaller overall footprint than a swing-arm design, at 60 pounds and 27 inch L by 26 inch W by 10 inch H, which matters if your bench space is already spoken for.
It taps M3 to M16 at up to 156 rpm with 200 N m of torque from a 600W servo. Stepless speed regulation and double torque protection combine servo-level torque control with chuck-level protection. The body is described as high strength, improving tapping precision and stability while reducing shake, and it reaches 43.3 inch horizontal and 21.5 inch vertical.
The single five-star review is emphatic. The buyer says to buy it, that it was worth every penny, and that it accepts standard tap collets including non-clutch collets. That last point is practical, because it means you are not locked into one collet brand.
Two limitations stand out. It runs on 220V, so a step-down transformer is needed on US circuits, and the 200 N m torque is the lowest published figure among the electric arms here, which leaves less margin on coarse threads. There is also only one review, which is thin evidence on long-term reliability.
Why the vertical format helps
When every part you tap has a hole in the top face, a vertical column machine is faster to set up than swinging an arm into position. The collet and controls sit together, so you load a tap and change a setting without walking around the machine.
The reduced vibration is the other argument. A rigid body means the tap stays on its own axis, which is the single biggest factor in thread quality on light machines.
Where it will disappoint
If your work includes overhead or side-facing holes, the vertical format forces you back to repositioning the part, which erodes the time saving you bought it for.
Torque headroom is limited. On hard steel at the top of the M16 range, plan on slower speeds and gentler feeds rather than pushing the cycle.
7. Pavrots M6-M36 Electric Tapping Arm – Widest Thread Range in the Group
Electric Tapping Arm & Tapping Machine M6-M36, 360° Multi-Directional, Automatic Lubrication & Air Blowing, 0-375RPM, 11 ISO Collets Included, AC 110V (M6-M36)
Capacity: M6-M36
Speed: 0-156 rpm listed
Working area: 1180mm x 400mm
Collets: 11 ISO
Pros
- Widest thread range here at M6 through M36
- Automatic oil spray lubrication and air blowing
- Vibration mode removes chips in deep holes
- Overload clutch separates before the tap is damaged
- Magnetic base option avoids drilling the bench
Cons
- Oil spray and air blow need an air compressor connection
- Title and spec block conflict on rotation speed
- Very large 60 inch by 60 inch listed footprint
Two machines in this roundup cover M6 to M36, and this is the one that adds pneumatic assistance. For structural steel, large flange bolts and pipe threads, that range is the whole argument, and the 1180mm horizontal by 400mm vertical working area gives you room to swing around a plate on the floor.
The features here are unusual. An oil-spraying function lubricates during tapping and air blowing loosens the finished thread, and both require a connection to an air compressor. A third working mode, Vibration, is built specifically for deep tapping with chip removal to protect tap life. The clamping cylinder carries an overload protection device where an adjustable safety clutch separates when torque exceeds its rating.
It also handles non-standard pitches, reverse-tightening connection threads, drive threads and pipe threads. The mounting base is fixed with M10 bolts at 100mm hole spacing, with a magnetic base offered as an option using pre-reserved screw holes, and 11 ISO collets are included.
Watch two details. The listing title claims 0 to 375 RPM while the specification block says 0 to 156 rpm, so confirm the real speed with the seller. The listed dimensions of 60 inch L by 13 inch W by 60 inch H also mean this needs real floor or bench space, and all four ratings carry no written review text.
Why large-thread buyers should look here
M24 and M36 threads on a fabricated frame or a pipe stub are the jobs that make people hand-tap out of desperation. Covering them on a powered arm removes the temptation.
Automatic lubrication and air blowing are genuinely useful at this scale. Cutting fluid delivered at the hole is what keeps a large tap from binding, and blowing the thread out on withdrawal helps seat the fastener.
Where it gets complicated
The air compressor dependency is real. If your shop has no compressor or an unreliable one, you lose lubrication and thread clearing, which are the two features that justify the size.
It also starts at M6, so it cannot serve a shop that also handles small electronic fasteners. Most shops end up owning one of these alongside a smaller M3 arm.
8. MXBAOHENG Pneumatic Tapping Gun – Best Low-Cost Entry Point
MXBAOHENG Pneumatic Tapping Machine M3-M12 Thread Tapping Gun 400 RPM
Capacity: M3-M12
Speed: 400 rpm
Power: air at 6-8 bar
Air use: 4 cfm
Pros
- Build quality exceeds expectations with real heft
- Forward and reverse control for tap withdrawal
- Accepts Lyndex-Nikken and metric collets
- Handled 1/2 inch NC taps in aluminium with proper feed
Cons
- Performance drops off on larger threads
- Stock blue inlet fitting is too restrictive
- Supplied collets are metric only
- No overload protection so a seized tap can snap
This is a pneumatic tapping gun rather than a complete machine, and that distinction matters. You are buying the head; the articulating arm and the compressor are separate purchases. At 400 rpm on 6 to 8 bar shop air with a 1/4 inch inlet and average consumption of 4 cfm, it is the cheapest real path into power tapping.
The build surprises people. Buyers call the quality solid, note it has real heft in the hand, and confirm it accepts Lyndex-Nikken imperial and metric collets as well as the supplied ISO Type 1 collets. One reviewer handled 1/2 inch NC taps in aluminium when fed by half-inch tubing at 120 psi.
The limits come from experienced users, and they are worth respecting. Performance drops off on larger threads, and the same buyer described half-inch NC in aluminium as a struggle. Results depend on quality spiral flute machine taps. The stock blue inlet fitting is too restrictive and should be swapped for a proper coupler, and the supplied collets are metric only.
Most importantly, there is no overload protection built in, so a seized tap can snap with no warning. If tap breakage is the reason you are shopping, this machine does not solve it.
Why it is worth considering
If your shop already has an articulating arm and a compressor, this is a small addition that turns hand tapping into power tapping. The ISO chuck is a standard size, so spares are easy to find.
Non-hardened work in aluminium, copper and iron is its sweet spot. Machine housings, end faces, nuts and flanges all fall inside that envelope.
Where it falls apart
There is no torque protection, and that is the reason experienced users do not use these on steel. If a tap binds, the torque goes straight into the tap rather than into a clutch.
You also need a genuine air supply. A small workshop compressor that cannot hold 6 to 8 bar will make the 400 rpm figure meaningless.
9. TX Pneumatic Tapping Arm – Best for Angled and Vertical Head Work
1000mm M3-M12 Pneumatic Tapping Machine Tapping Tool Drilling Threading Machine Air Tapper with 6 Chuck 360° arm 90° Head
Capacity: M3-M12
Head: 90 or 360 degree
Arm: 1000mm
Protection: overload and over-voltage
Pros
- Six chucks cover the full M3 to M12 range
- 360 degree arm with a choice of 90 or 360 degree head
- Over-voltage over-current and over-load protection
- Tap protection for through-hole and blind-hole tapping
Cons
- The only customer review is several years old
- leaving reliability unverified
- Bullets describe an electric machine while the title says pneumatic
- No published air pressure or power figures
This pneumatic arm comes with six chucks covering M3, M4, M5, M8, M10 and M12, which is the most complete collet package for that range in the pneumatic group. You are not hunting for a size you do not have on day one.
The head is the distinguishing feature. Variants are offered with a 90 degree rotary head on a 360 degree arm, or a 360 degree rotary head on the same arm, and the arm itself is 1000mm. That lets you tap vertically into a workpiece on the bench or swing around to an angled face depending on the part. The arm supports a vertical or universal working direction.
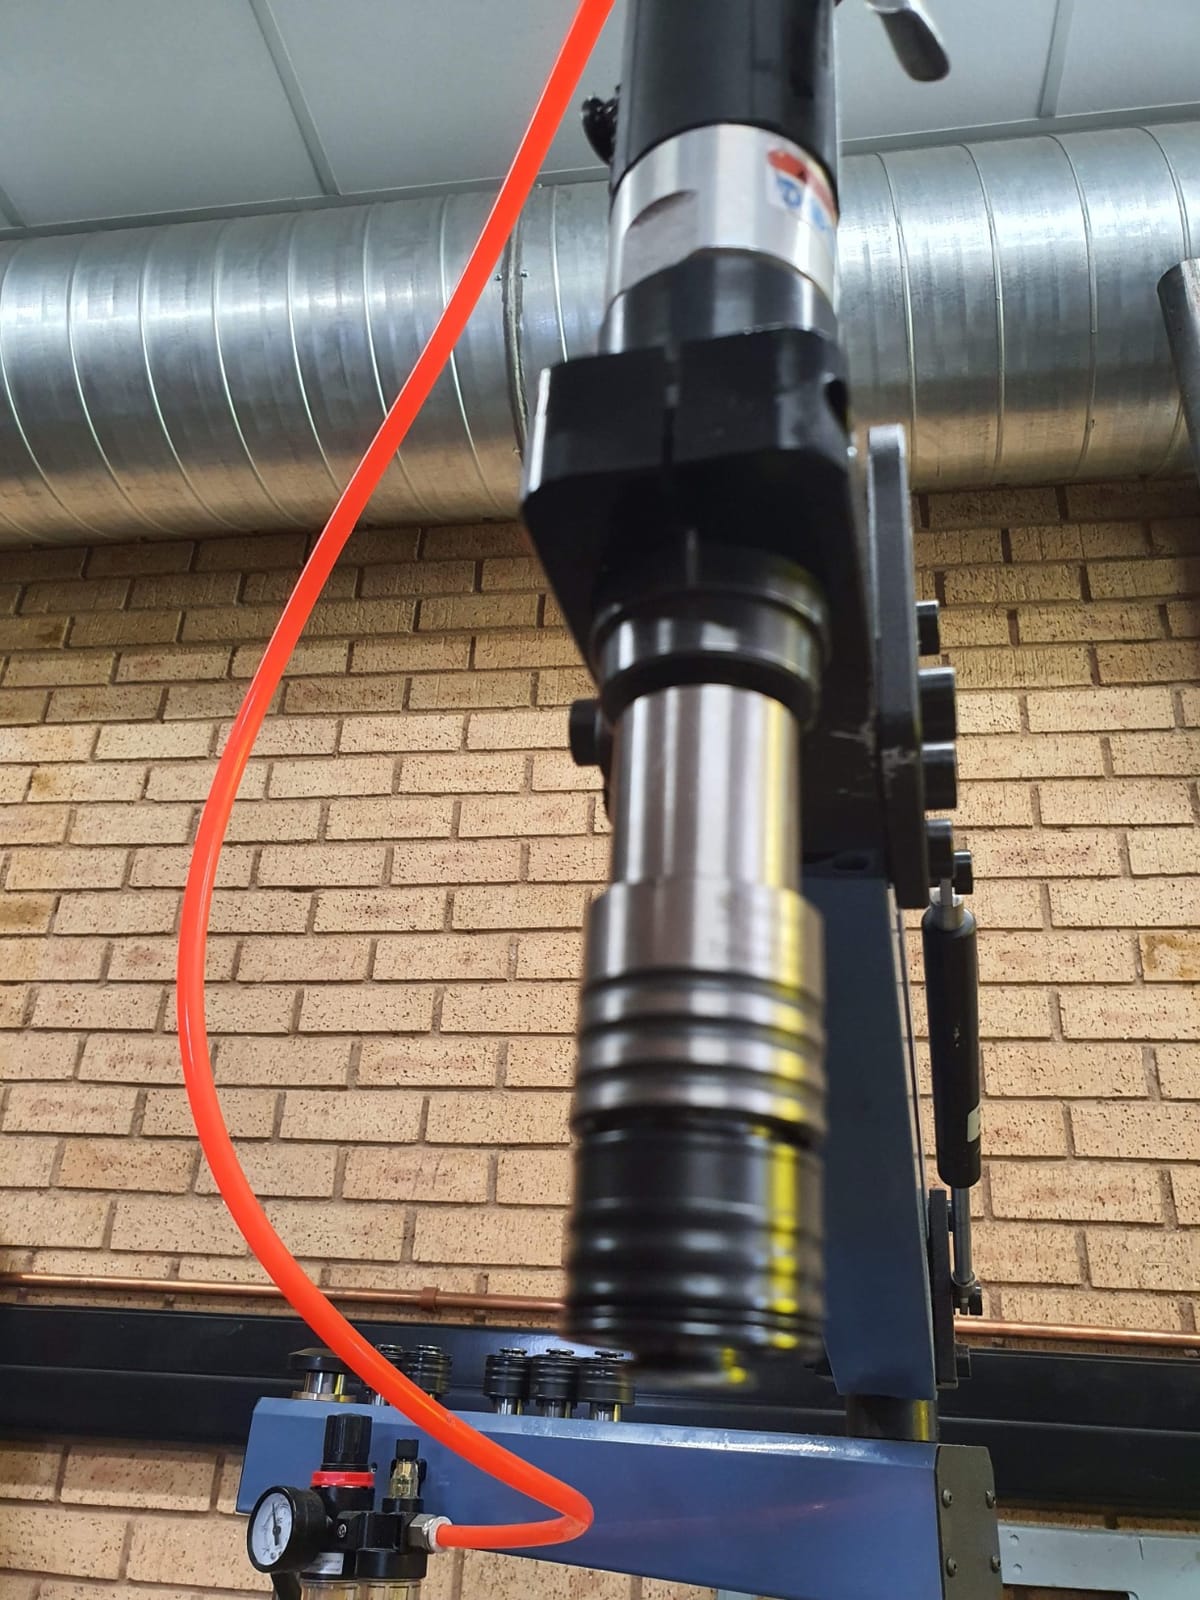
Protection is specified as over-voltage, over-current and over-load, plus dedicated tap protection for through-hole and blind-hole tapping. A touch layer design gives automatic or manual modes, and the head runs high speed with low torque or low speed with high torque.
The listing itself is the weak point, and buyers should be aware of it. The feature bullets describe an electric tapping machine while the title specifies a pneumatic air tapper, and no air pressure, RPM or power consumption is published, so compressor sizing is guesswork. The only review comes from a factory buyer and is several years old, which says more about intent than about longevity.
Why the head options matter
When your parts are fabricated brackets and covers rather than flat plate, a 90 degree head can reach an angled face without rotating the workpiece off the fixture. That is where an arm design earns its extra cost.
The six included chucks mean a shop covering M3 through M12 covers the overwhelming majority of sheet-metal and enclosure fastening.
Where you need to ask questions
Before buying, get the air pressure, the free air delivery in cfm, and the motor power in writing. Without those numbers you cannot tell whether your compressor can run it without bogging down.
Resolve the electric-versus-pneumatic contradiction with the seller. Which one you are actually receiving matters for how you plumb the shop.
10. Sevencow Mechanical Hot Tapping Kit – for Live Pipe, Not Threads
08350 DM3MECH Hot Tapping Machine Kit 3/4-4″ Valves 300 PSI NPT
Valve range: 3/4 to 4 inch NPT
Pressure: 300 psi ambient
Power: manual mechanical
Weight: 4.74 kg
Pros
- Complete kit with every part needed for the job
- Taps live piping so no shutdown drain or refill
- Works across steel copper brass and aluminum
- Includes hole saws and arbor
Cons
- No instructions included so it is only usable if you know the technique
- Packing gasket can arrive hard and brittle
- Excess force on breakthrough can damage the retainer
We include this kit because it is often mistaken for a tapping machine, and it is not one. It drills into a live, pressurized pipe to fit a branch connection, but it does not cut screw threads. If you came here looking for internal threads, this is not the tool.
What it does is genuinely useful in a different trade. It hot taps steel, copper, brass or aluminium pipe to install a branch from a 3/4 inch to 4 inch valve without shutting down, draining, cutting, refitting and refilling the system. Pressure rating is 300 psi at ambient temperature and 15 psi for steam systems.
Reviews are mixed at 4.3 stars across four ratings. One buyer confirms it is a complete kit that worked well on their project, while flagging that there are no instructions and you need to already know how to use it. Another buyer rated it three out of five because the packing gasket arrived hard and brittle.
There is a safety detail that matters more than any spec here. Applying excessive force while cutting the coupon can cause sudden breakthrough that drives the retainer into the back of the main and damages it. The prevention is to cut a 3/4 inch copper tube spacer long enough to stop the retainer hitting the back, slipped over the exposed shaft. It is also not recommended for ammonia, gas or other caustic systems.
Why a metalworker should still know it exists
If your shop maintains hydraulic, compressed air or cooling water piping, this saves a shutdown window you may not have. That is a real operational saving on a plant where you cannot stop the line.
It works across four common metals, so a mixed-material piping run is not a problem.
Where it does not apply
It will not produce a threaded hole. If your requirement is an M8 or M10 internal thread for a fastener, none of this applies and you want one of the tapping arms above.
No instructions ship with the kit, and the technique has a real learning curve. Do not practise on a live pressure line you cannot afford to replace.
11. DEJUN Pneumatic Tapping Machine – Best All-Round Pneumatic Arm
DEJUN Pneumatic Tapping Machine, M3-M12 Air Tapper with Taps and Collets
Capacity: M3-M12
Speed: 400 rpm
Torque: 70 N m
Arm radius: 1000mm
Pros
- Taps and collets included so it is usable out of the box
- Clamping cylinder overload protection with adjustable safety clutch
- Oil-water separator keeps supply air clean
- 360 degree folding arm with 1000mm working radius
Cons
- No compressor pressure or airflow specification is published
- 70 N m torque is modest next to the electric arms
- No written user reviews beyond star ratings
This is the pneumatic machine to buy if your shop already runs a compressor, and it comes with taps and collets included, so you can run work on the day it arrives. Seven buyers rate it 4.7 stars, the strongest showing among the pneumatic units here.
It stands out from the cheaper pneumatic gun on two points. The clamping cylinder carries an overload protection device with an adjustable safety clutch that separates when tapping torque exceeds the rated value, and the oil-water separator removes oil and water from the supply air, which is what keeps the motor running consistently over time.
The body is a high-strength aluminum alloy with a folding arm that rotates 360 degrees on the workbench and taps vertically, giving a 1000mm working radius. The pneumatic motor runs at 400 rpm and covers copper, iron, aluminium, steel, stainless steel, plastic and wood. The application list runs to machinery, moulds, packaging equipment, automobile and motorcycle parts and aviation components.
Two limits are worth stating plainly. The torque rating is 70 N m, roughly a third of what the 600W electric arms deliver, so this suits light to medium work rather than large threads. And no compressor specification is published, meaning you have to size your air supply yourself. None of the seven ratings include written commentary.
Why pneumatic still makes sense
A pneumatic motor is simple, cool-running and does not need a transformer or a dedicated circuit. For a shop that already has a compressor, that removes real installation friction.
Including taps and collets is a genuine saving at the start. You are not searching for a matched collet set before your first part.
Where electric wins
At 70 N m, hard steel and coarse-pitch threads are outside this machine’s comfort zone. If your work is mostly 304 stainless or mild steel structural work, an electric arm gives you more headroom.
The missing compressor figures are a genuine planning gap. Confirm your air supply delivers at the required pressure and flow at the machine, not just at the receiver.
12. LYXC M6-M36 Electric Tapping Machine – Long Reach for Plate Work
M6-M36 Tap Collets 1200mm Arm 360° Universal Tapping Machine Electric Tapper 125rpm
Capacity: M6-M36
Motor: 1200W
Speed: 125 rpm
Reach: 1200mm horizontal
Pros
- One owner says every shop needs one and saved threading costs in-house
- 1200W motor handles large M6 to M36 threads
- Longest reach among the arms here at 1200mm
- Triple balanced aluminum arm for precise hole alignment
Cons
- 220V supply requires a step-down transformer
- Heaviest unit at 120.7 pounds so it is a two-person lift
- Fixed 125 rpm with no stepless regulation
- Only one customer review and it is dated
This machine covers M6 to M36 with a 1200W motor and a 1200mm horizontal working radius, the longest reach among the arms in this roundup. That combination suits plate work, where holes sit far apart and you would otherwise reposition the machine between every tapping point.
The arm is a triple balanced articulated design made entirely of aluminum, described as fast and precise in hole alignment. The HD human-machine interface adjusts forward and backward speed independently, and the adjustable clutch covers both blind and open holes. Rotation speed varies according to tapping diameter, with maximum counterclockwise speed for fast tool output.
The single five-star review makes the economic case rather than the technical one. A working shop owner says it is worth every penny, that every shop needs one, and that it saved so much money threading plates in-house that they no longer send that work out to a machine shop. The material list spans aluminium, copper, A3 steel, 45 steel, cast iron, Q235, S136, mold steel, 718H, 40Cr and stainless steel.
Four practical drawbacks. It runs on 220V, so a step-down transformer is required on US circuits. At 120.7 pounds it is the heaviest unit here and effectively a two-person lift. Rotation is a fixed 125 rpm with no stepless regulation listed. And a single customer review is thin evidence for a machine this size.
Why reach matters for plate work
On a large plate, the tap rarely sits where the machine is. A 1200mm radius removes the repositioning between holes, and that is where the reported time savings come from.
The triple-balanced arm is not a cosmetic feature. Alignment is what keeps a large tap on axis, and misaligned large taps are the ones that snap.
Where it falls short
The weight is a real logistics issue. Getting 120.7 pounds onto a bench or a floor position needs two people and a clear path.
Fixed speed means you cannot optimise per material the way you can on a stepless machine, so soft aluminium and hardened steel will both run at a compromise.
How to Choose a Tapping Machine for Your Shop
Work through these in order, and the choice makes itself before you start comparing brands.
1. Match the largest thread you actually tap. Buy capacity above your current maximum, not at it. An M3 to M16 arm covers most sheet-metal and enclosure work, an M3 to M24 arm covers structural work, and an M6 to M36 arm is a large-plate machine. Buying a machine that only covers M3 to M12 means a second purchase the first time a job lands above that.
2. Check torque, not just speed. Headline RPM matters far less than the torque available at low speed, because that is where the cutting resistance lives. Published figures in this group run from 70 N m on the pneumatic arm to 256 N m on the 600W electric machine.
3. Confirm the torque protection exists. A torque collet chuck or an adjustable safety clutch is what stops a bind from becoming a snapped tap. Several pneumatic guns on the market have neither, and experienced machinists on forums consistently rule those out for steel.
4. Look at reach before you look at features. Measure from where the machine will sit to the furthest hole. A 1000mm arm covers a bench, a 1200mm arm covers plate work, and an arm that is too short turns every job into a repositioning exercise.
5. Match the drive to your shop. Electric arms run on 110V or 220V and give more torque. Several of the best-rated models here are 220V only, so a step-down transformer is part of the install. Pneumatic machines need a compressor delivering steady pressure and flow. A benchtop vertical machine is faster to set up but only handles top-down holes.
6. Check whether it drills. Most machines here tap only. Two list a metal drilling capacity: the TECHTONGDA at 16 millimeters and the INTBUYING at 0.63 inches. Everything else needs a separate drill press or mill, and our guide to the best floor drill presses for metalworking covers the pilot-drilling side of the job.
Can a drill press tap?
Yes, for small threads in forgiving material, and buyers on r/metalworking describe it as workable for A572 in the M6 to M10 range with slow steady feeds, cutting oil and a rigid setup. The catch is that a drill press has no synchronized feed, so the operator is the synchronization. That is exactly why taps break. If you are setting up a fabrication workflow, a proper machine is the difference between occasional tapping and repeatable tapping. Our floor drill press roundup makes the same case for the drilling side of the shop.
Tapping head retrofit or standalone machine?
If you already own a rigid mill, a mill-mounted tapping head is the economical choice for volume work, and experienced users on cnczone and polytechforum consistently describe the Procunier as fast, reliable and not prone to breaking taps. If you do not own a mill, or your holes are spread across different parts and positions, a standalone tapping arm is the correct answer. Experience on the same forums separates the two cleanly: a head for high volume on a machine you own, an arm for flexible low-volume work with no mill in the shop.
What type of tap is best for power tapping?
Match the tap geometry to the hole, not the machine. For through-holes use a spiral point or gun tap, which pushes chips forward out of the hole. For blind holes use a spiral flute tap, which lifts chips out of the hole and will survive the depth. For soft ductile material such as aluminium and mild steel, a form tap produces the strongest thread and lasts longest, but it needs a precise hole and it cannot tolerate a chip in the bottom. For high-volume work on the same hole, roll taps are worth the setup cost, and buyers on cnczone recommend them for large runs of small threads where form taps wear out. In every case, match the tap to the machine’s collet size and confirm the machine’s depth capability exceeds the hole depth before you start.
How to Tap Steel Without Breaking Taps
Tap breakage is the single most cited fear in metalworking forums, and it is the right criterion to shop on. Most breaks come from the same three causes: the tap is being fed faster than it cuts, the hole is generating heat and work hardening the tap, or the torque clutch is set too high for the thread.
Slow the feed to match the tap. This is the whole principle of a synchronized machine, and on a manual setup it means watching the tap rather than the dial. A tap that has to be pushed is a tap that is being overloaded.
Use cutting fluid on every steel operation. Flood the hole, not just the entry. The fluid’s job is to carry heat away and clear chips, and it makes the single biggest difference to tap life in steel.
Peck in blind holes. Advance until chips clear, retract fully to break the chip, and repeat. Leave a little less depth than the hole depth so the tap never bottoms out, because a tap that reaches the bottom of a blind hole has nowhere to go and will twist off.
Set the torque clutch for the tap, not the machine. A clutch set for M12 will happily snap an M6 tap. Re-adjust it each time you change size, and on machines where the clutch lives on the tool holder, expect to do this on every changeover.
Slow the return for soft metals. Aluminium and 304 stainless grab on withdrawal, and a lower reverse speed reduces that risk. Several machines in this roundup let you set reverse speed separately, and that is a feature worth paying for if those are your materials.
Finally, verify thread fit before you run a batch. A Go/No-Go gauge tells you in seconds whether the thread matches its class, and catching one bad hole now beats discovering it at assembly.
Frequently Asked Questions
What are the different types of tapping machines?
There are seven main classes: electric tapping arms, pneumatic tapping arms, hand-held pneumatic tapping guns, bench or tabletop tapping machines, CNC drilling and tapping centers, magnetic-base tapping machines and tapping head retrofits for a mill. Electric arms are the general-purpose choice for small shops, pneumatic units suit shops that already run a compressor, CNC centers suit batch volume, and a retrofit head suits shops that already own a rigid mill.
What type of tap is best for power tapping?
Match the tap to the hole. Use spiral point or gun taps for through-holes so chips are pushed forward out of the opening. Use spiral flute taps for blind holes so chips are lifted back out and the tap does not pack the bottom. Form taps give the strongest thread in aluminium and mild steel but need a precise hole. Roll taps are worth the setup for high-volume runs of the same small thread size.
Can a drill press tap?
Yes, for small threads in forgiving material. Machinists describe tapping M6 to M10 in A572 steel in a drill press as workable with slow steady feeds, cutting oil and a rigid setup. The limitation is that a drill press has no synchronized feed, so the operator controls the match between tap rotation and feed rate, and that is the main reason taps break. Above those sizes, or in stainless and hardened alloys, use a dedicated machine with a torque clutch.
Is a tapping machine worth it compared with tapping by hand?
For a shop tapping more than a few holes a week, yes. Buyers report cutting tapping time by around half and breaking far fewer taps, and the machine removes the wrist and arm load that makes hand tapping inconsistent. For occasional work on small fasteners in soft material, a good tap wrench and the correct tap geometry are still cheaper and adequate.
What tap size does a tapping machine handle?
It depends on the class. Hand-held pneumatic guns in this group cover M3 to M12. Electric tapping arms commonly cover M3 to M16, mid-range arms cover M4 to M24, and large electric arms cover M6 to M36. Buy capacity above your largest current thread, and confirm the collet set includes the sizes you use rather than assuming the machine and the collets match.
Should I choose an electric or a pneumatic tapping arm?
Choose electric if you tap steel, stainless or threads above M12, or if you want more torque and no compressor dependency. Choose pneumatic if your shop already has a compressor delivering steady pressure and your work stays in aluminium, copper and mild steel at M12 and below. Several strong electric models are 220V only, so a step-down transformer is part of the install either way.
Conclusion
The best tapping machines for metalworking in 2026 come down to one honest question: how large are your threads, and how much steel do you cut. For a small fabrication shop tapping M3 to M16 regularly, the XINCHENG PRECISION electric arm takes the top slot, with stepless 0 to 375 rpm control, a safety torque collet, automatic reverse and enough user feedback to judge it fairly. For repeat production work with the largest body of written feedback, the WTTTOOLS arm halves tapping time for its buyers.
Work larger than M16? The M4 to M24 arm or one of the M6 to M36 machines covers structural and plate work. Already have a compressor and stay in aluminium? The pneumatic options are cheaper and simpler.
Check the torque protection exists before you pay, because that single feature decides whether you are still buying taps next year. If you are also building out the metal side of the shop, our floor drill press roundup covers the pilot-drilling side, and our beginner welding machine guide covers the fabrication steps that usually come before tapping.
Machine tools age fast, so verify the current specification with the seller before you commit, and if you are building out a fabrication shop alongside a welder, confirm the transformer requirements and socket amperage before the machine arrives. That single pre-purchase check avoids the most common installation regret in this whole category.